
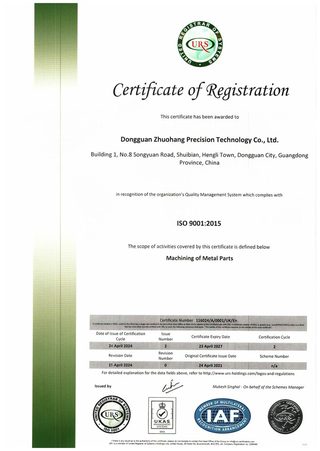
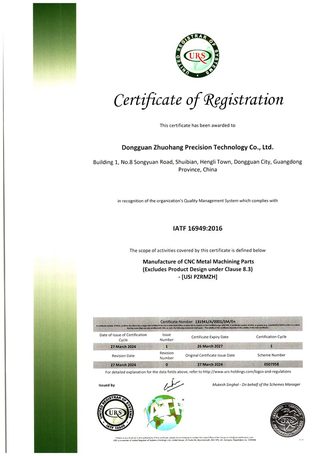
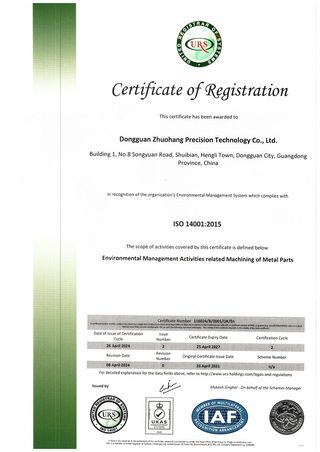
- Three certificates — ISO 9001, IATF 16949, ISO 14001 — held by Dongguan Zhuohang Ltd, verifiable with URS.
- Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a 76.1–76.5 mm length characteristic, against an initial-study target of Ppk ≥ 1.67.
- Hexagon CMMs + XRF + SPC — the measurement, not the marketing.
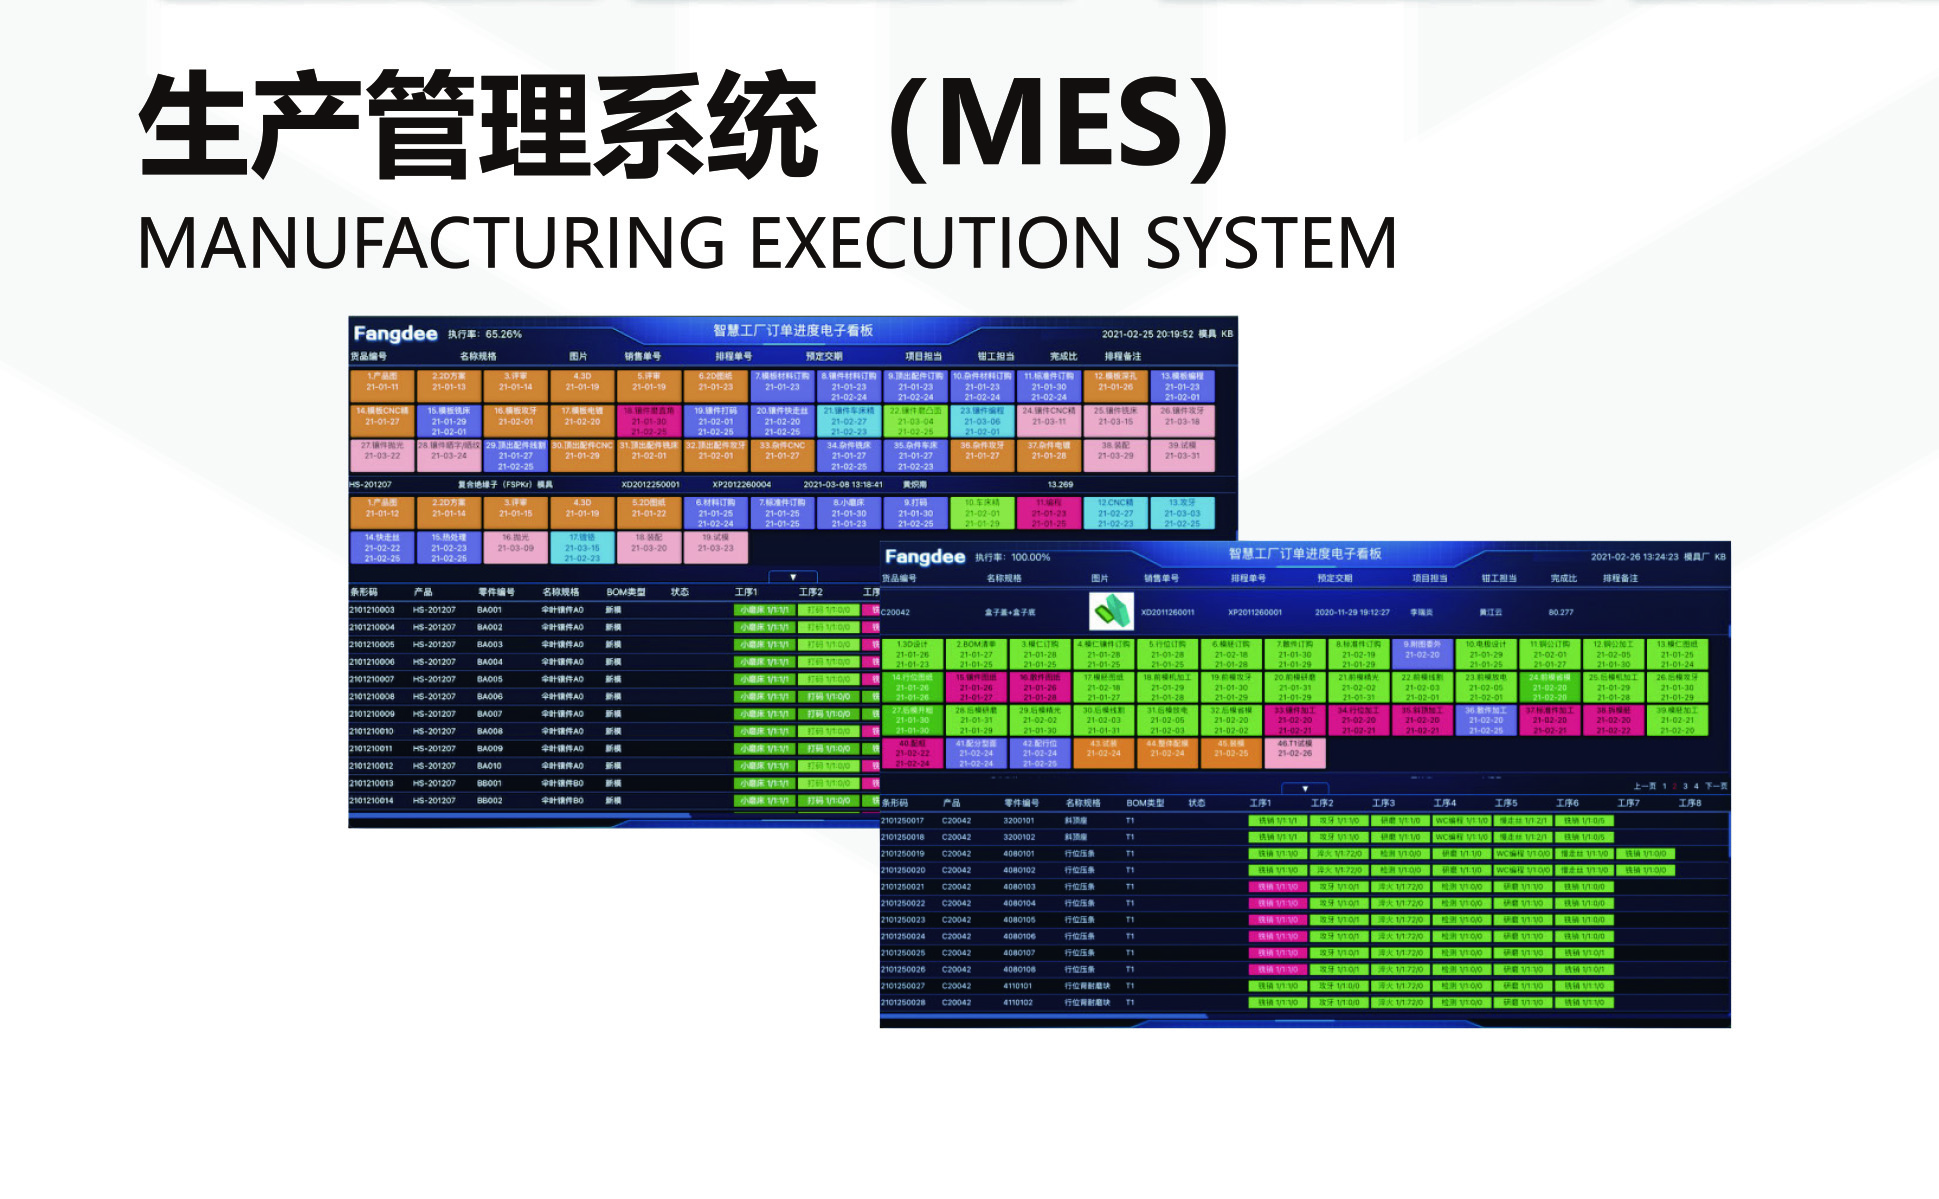
- Full lot traceability from raw material to shipment via MES/ERP.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
How do you audit a machining quality system?
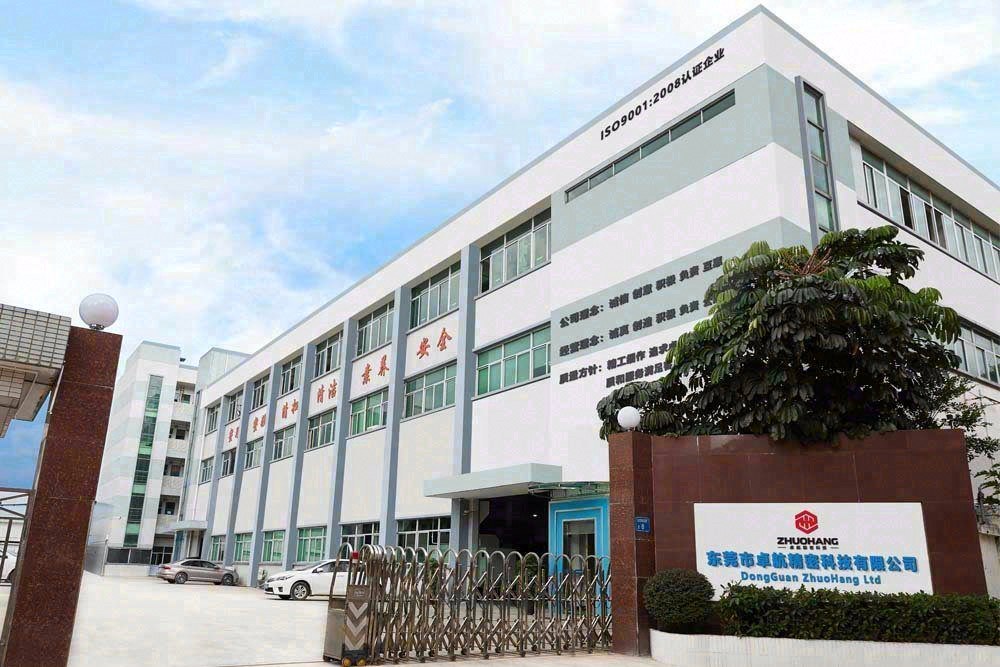
A quality system is audited the same way a part is inspected: against evidence, not claims. The checklist has four layers — certification, measurement, process control, and traceability. A supplier that can document all four has done most of the work a buyer would otherwise have to do by flying there.
The sections below walk each layer, with the specific evidence this factory provides. The principle throughout is the same: a number you can check beats an adjective you cannot.
The four layers answer four different questions. Certification answers "does a third party believe the system exists." Measurement answers "can the shop actually verify a dimension." Process control answers "does the process stay put over the run." Traceability answers "can you find the bad lot if one escapes." Skip any one and the quality story has a hole in exactly the place your part will eventually fail.
Which certificates back the system, and how do you verify them?
Certificates are the cheapest pre-audit, because a third-party registrar already did the work. They protect a buyer only if they are real, current, and held by the entity that invoices, so the names and numbers below are given precisely, the way an auditor would want them.
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3 — this is a build-to-print manufacturer. Every number above is held by Dongguan Zhuohang Ltd and verifiable with the registrar URS. You can and should check each one independently.
Read the scope against the work you are ordering. ISO 9001 says a quality system exists; IATF 16949 says the automotive discipline — SPC, PPAP, PFMEA, traceability — is in place; ISO 14001 says environmental management is audited too. The certificate that matters is the one whose scope covers your part, not the one with the most logos.
How is process capability actually measured?
A "capability statement" is a promise; an SPC chart is evidence. This factory runs statistical process control on key characteristics and states the number plainly, with the measurement behind it.
On a representative length characteristic of 76.1–76.5 mm, over 25 subgroups, process capability measured Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) — against a key-characteristic target of Ppk ≥ 1.67 initial and a general-characteristic target of Cpk ≥ 1.33. A real CMM report and SPC chart for a past job are available on request. That is the document to ask for in an audit, not the "we hold tight tolerances" line.
The subgroup count matters because process capability is a statistical claim, not a single measurement. One part in spec proves nothing; twenty-five subgroups of parts staying in spec, with the spread characterized, is what the Cpk number actually summarizes. Ask for the chart behind the number.
What inspection equipment verifies the parts?
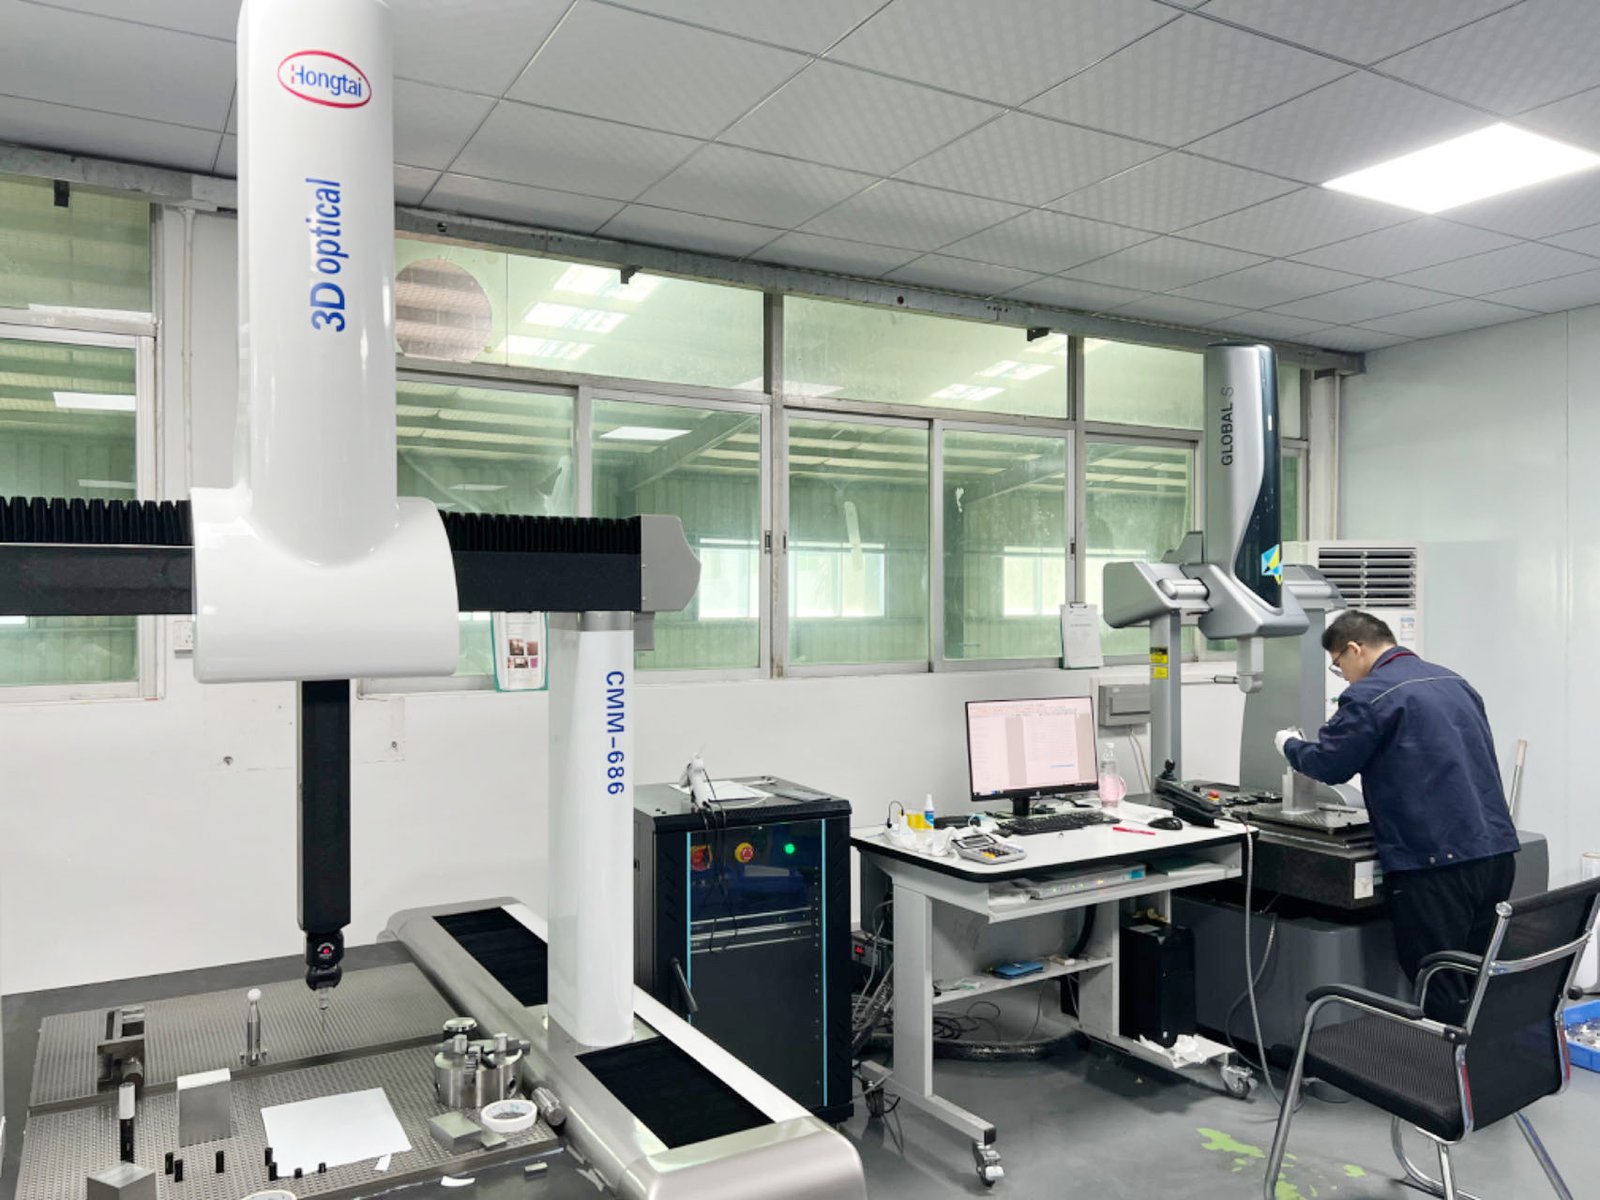
The measurement is only as good as the instruments behind it. The inspection bench here is the same class of equipment a buyer would use to audit the shop:
- Two Hexagon GLOBAL S CMMs, a gear measuring center (ZD20), and vision measuring machines for dimensional verification.
- KEYENCE VK-X3000 laser microscope and SURFCOM 1800D for surface finish and profile.
- XRF (iCHEQ) spectrometer for incoming material composition checks against the mill certificate.
- HVS-1000A micro-Vickers hardness tester, Fischer coating thickness gauge, salt spray and tensile testers, plus Mitutoyo and TESA height gauges.
The list reads as coverage, not as decoration: dimensions, surface finish, material composition, hardness, coating, and corrosion each have an instrument. A part leaves only after the dimension it depends on was measured on the instrument made for it, which is what separates an inspection bench from a shelf of gauges.
Does the system support PPAP and APQP?
For automotive and regulated buyers, the question is whether the shop can produce the documentation package, not just the parts. This factory has produced a complete automotive-grade quality package for a customer program:
- Process flow chart — incoming inspection through machining, post-processing, and shipment.
- Control plan — critical characteristics, tolerances, speeds/feeds, and sampling frequency.
- SPC — control charts with the Cpk calculation above.
- PFMEA — failure modes with severity, occurrence, detection, and RPN.
- Environmental control procedures — noise, waste water, and air.
That is APQP and PPAP capability demonstrated on a real program, available as evidence rather than as a claim.
How is material and part traceability handled?
Traceability is what turns a rare defect from a mystery into a manageable event. Two controls run on every lot here. First, incoming material is XRF-checked against the mill certificate, so a mixed or substituted lot is caught at the door. Second, the MES/ERP system records the full chain — raw material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results. If a non-conformance ever surfaces, the answer is specific: which lot, which machine, which operator, and the impact can be isolated instead of guessed.
The value of the full chain is that it converts a recall into a recall of one lot. Without it, a defect in a thousand-part order means a thousand parts are suspect; with it, the record narrows the exposure to the exact batch that ran the bad setup. Traceability is not paperwork for its own sake — it is the difference between containing a problem and eating an entire order.
What reports ship with the parts?
Documentation is your half of the quality system. With every shipment, the parts are accompanied by CMM inspection reports, SPC charts, and material certificates — evidence of what was made and measured, not a pass/fail line. A first-article inspection report is available before volume is released, so a problem is caught while it is still cheap to correct.

The reason the documents travel with the parts is that your incoming inspection is the last line of the audit. When the CMM report, the SPC chart, and the material cert arrive with the shipment, your inspector is checking against the shop's evidence rather than starting from zero. That is the practical difference a documented shop makes on the receiving dock.
How do you verify these claims for yourself?
Do not take the claims on this page as settled — treat them as checkable, and check them. Three requests settle it: the certificate numbers (verify with the registrar), a real CMM report from a past job (not a capability statement), and a live walk-through of the inspection bench. A supplier that provides all three on the first exchange is the tier you wants; one that stalls has told you its tier.
- Certificate in another entity's name? It is not your certificate.
- "Passed" instead of a CMM report? There is no measurement to audit.
- No Cpk number, or a number with no chart? The capability is unproven.
- No PPAP/APQP package for automotive? The quality system stops at the part.
What does a Cpk number actually mean?
Cpk is the number that tells a buyer whether the process can stay inside the tolerance, not just whether one part did. It measures the distance from the process mean to the nearest specification limit, divided by the process spread, so a high Cpk means the mean is far from the limit relative to how much the process wanders.
The thresholds are a rough ladder. A Cpk of 1.33 corresponds to a process whose spread fits about four times inside the tolerance band — the usual floor for a general characteristic. A Cpk of 1.67 is about five sigma, the target for a key characteristic that cannot be allowed to drift. A Cpk of 2.0 is six sigma, effectively no rejects from a stable process. The factory's Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) sits above the key-characteristic target, which is what the SPC chart on the 76.1–76.5 mm characteristic demonstrates.
The audit point is not to memorize the math but to ask for the chart. A Cpk number without a control chart behind it is a decoration; a chart with a Cpk attached is a process you can hold a supplier to. The number and the chart travel together, or neither is worth anything.
How does measurement traceability work?
A CMM report is only as strong as the calibration behind the CMM, and calibration is only meaningful if it traces to a standard someone else holds. The chain runs upward: a shop gauge is checked against a working standard, the working standard against a laboratory reference, the reference against a national standard, and the national standard against the international system of units.
Each link in that chain has a certificate, and a shop that keeps its calibration certificates can show the tolerance claim is anchored, not floating. The audit questions are concrete: which CMM took the reading, when was it last calibrated, and is the calibration certificate available, and the same for the hand instruments, because a dimension is only as trustworthy as the least-traceable tool in the chain.
This factory runs its verification on Hexagon CMMs on a documented calibration cycle, with the calibration evidence offered alongside the inspection reports. That is the difference between a number you can act on and a number you take on faith, and it is one of the cheapest checks in the whole audit.
What is a PPAP package, and when do you need one?
PPAP — Production Part Approval Process — is the documentation package you require before a supplier is released to run production volume. It exists so you can confirm the process, not just the sample, before the order scales. The package assembles the evidence that the design, the process, and the measurement are all locked and documented.
The package pulls together the documents already described on this page: the process flow chart, the control plan, the PFMEA, the SPC study, the dimensional report, and the material and performance evidence. A buyer that requires PPAP is asking for the whole quality story in one file, so the decision to release volume is made on documents rather than on a pilot order.
When do you need one? When the part carries safety, regulatory, or recall risk — automotive and medical most obviously, but any buyer whose part cannot fail quietly. The audit question is simply whether the shop has produced the package before and can produce it for your program. This factory has, and the package is available as evidence, not as a promise.
How does a non-conformance get corrected?
A quality system is tested not by how it handles a good lot but by how it handles a bad one. When a non-conformance surfaces, the response follows a structured path: contain the lot, find the root cause, put a corrective action in place, and verify the fix holds over the next runs.
The traceability record is what makes that path fast. Because the MES/ERP system records the lot, the machine, the operator, and the inspection results, the investigation starts at the exact batch that went wrong instead of re-testing the whole order. The fix then targets the cause — a worn tool, a missed offset, a mis-set datum — rather than the symptom.
The audit question is whether the shop can show a closed corrective-action record from a past non-conformance. A shop that can is a shop that has already learned from a failure on someone else's order; a shop that says "we never have rejects" is a shop that either is not measuring or is not telling. Every real floor produces rejects; the quality system is what happens next.
What this shop actually runs
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Made for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Made for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Made for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Made for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Made for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Audit the quality system before the first order.
Send your drawing to [email protected] or call +86 13126536955, and request the certificate numbers, a real CMM report, and a live walk-through of the inspection bench.
Frequently Asked Questions
Which certifications back the quality system?
In short, ISO 9001:2015 (No. 116024/A/0001/UK/En), IATF 16949:2016 (No.
How is process capability measured?
In short, With SPC control charts on key characteristics. On a representative length characteristic of 76.1–76.5 mm, process capability measured Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), against an initial-study target of Ppk ≥ 1.67 on key characteristics and a production target of Cpk ≥ 1.33.
What inspection equipment verifies the parts?
In short, Two Hexagon GLOBAL S CMMs, a gear measuring center, and vision measuring machines for dimensions; a KEYENCE VK-X3000 laser microscope and SURFCOM 1800D for surface finish; an XRF spectrometer for material composition; plus hardness, coating thickness, salt spray, and tensile testers.
Does the quality system support PPAP and APQP?
In short, Yes. A complete automotive-grade quality package — process flow chart, control plan, SPC, PFMEA, and environmental control procedures — has been produced for a customer program, demonstrating APQP and PPAP capability for buyers who require it before volume release.
How is material traceability handled?
In short, Every incoming lot is XRF-checked against its mill certificate before machining, and an MES/ERP system records the full chain — raw material source and usage, process parameters, machine data, batch, operator, and inspection results — on every lot, so a non-conformance can be isolated to the exact lot and machine.
What reports ship with the parts?
In short, CMM inspection reports, SPC charts, and material certificates accompany the shipment, so you receive documented evidence of what was made and measured, not just a pass/fail line. First-article inspection reports are available before volume is released.
How do I verify the quality claims?
In short, Request the certificate numbers and check them with the registrar, ask for a CMM report from a real job rather than a capability statement, and request a live walk-through of the inspection bench. A supplier that provides all three on the first exchange is the tier you wants.
What does a Cpk number actually mean?
In short, Cpk measures how far the process mean sits from the nearest specification limit, relative to the process spread. A Cpk of 1.33 corresponds to a roughly four-sigma process, 1.67 to five sigma, and 2.0 to six sigma.
How does a non-conformance get corrected?
In short, Through a structured corrective-action process: contain the lot, find the root cause, put a corrective action in place, and verify it holds. The MES/ERP record localizes the issue to the exact lot, machine, and operator, so the fix targets the cause rather than the symptom.
China CNC Machining Quality — Related Pages
Continue reading: 3 Axis China CNC Machining · 4 Axis China CNC Machining · 5 Axis China CNC Machining
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars