
Defining Edm Spark Erosion Machine for China CNC Machining
On edm spark erosion machine, your interest is practical: what does this mean for cost, lead time and risk on your part? The honest answer depends on geometry and volume, not on a slogan. A capable shop states the trade-off plainly, which process reaches your features in the fewest setups, holds your true tolerances, and scales to your quantity.
Zhuohang Precision Machining Factory approaches every inquiry from that angle: 100+ CNC machines, ISO 9001:2015 · IATF 16949:2016 · ISO 14001:2015, and a single engineering contact so the answer does not get lost between sales and the floor.
Process & Equipment Options
Design for manufacturability is where part cost is won or lost. The principles are boring and non-negotiable:
- Internal corners cannot be sharp — an end mill leaves a radius. Call out a fillet (≥ 0.5 mm) instead of a square corner.
- Hole depth should stay near or below 4× the diameter for twist drilling; deeper holes need gun drills and longer lead times.
- Walls thinner than ~0.5–1.0 mm chatter and distort. Thicker is cheaper and more stable.
- Standard threads under ~M2 / #2 are fragile in soft metals — avoid unless the assembly demands them.
- Tight tolerances cost money on every feature. Tighten only the surfaces that mate or seal; leave the rest at ISO 2768.
- Heat-treated parts move. If flatness matters post-hardening, plan a finish-grind operation and say so in the RFQ.
Good DFM is not about dumbing the design down — it is about spending tolerance and features only where the product actually needs them.
Quality Control and Inspection
Before you send the RFQ, run this five-point check:
- Is every tight tolerance tied to a function, or habit?
- Did you name the exact material grade and any cert?
- Are internal corners filleted (no square corners from end mills)?
- Is hole depth within ~4× diameter, or do you need a specialty drill?
- Do you need FAI/PPAP, and did you say so?
EDM spark erosion — the undercut and the hardened-steel corner that milling cannot reach

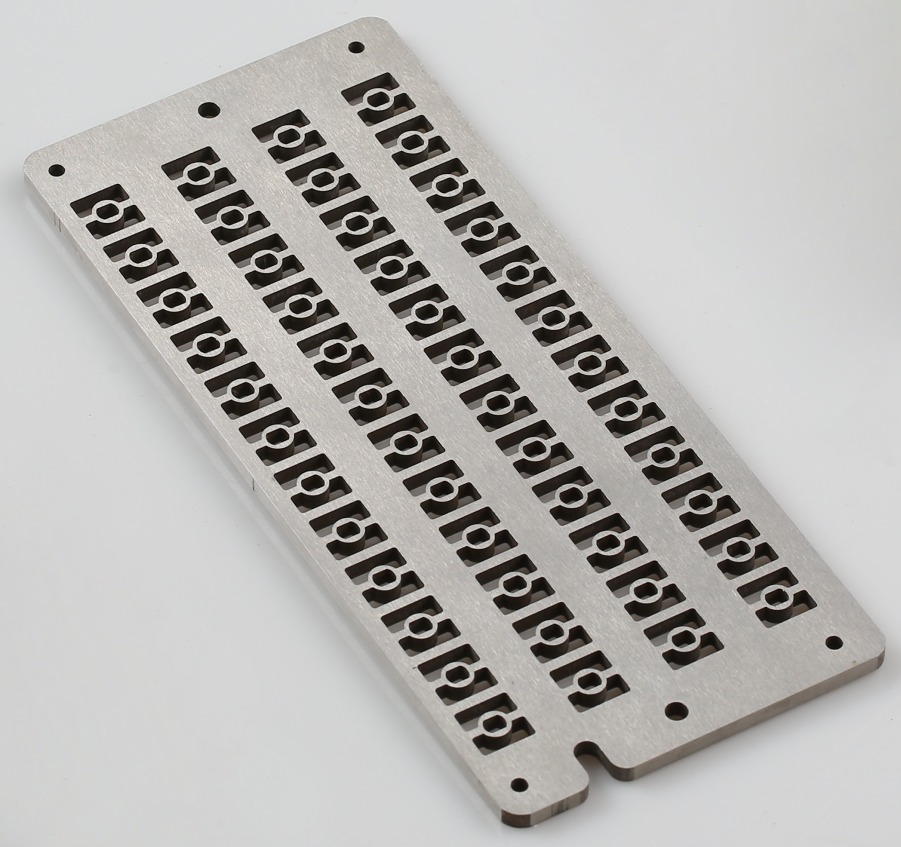
EDM — Electrical Discharge Machining, spark erosion — is the process that cuts conductive material with a spark, and the spark reaches geometry that a milling cutter cannot. A milling cutter is round, so it leaves a radius in every internal corner; an EDM wire or electrode cuts a sharp internal corner, a feature with an undercut, or a profile in hardened steel that would destroy a milling tool. If you need a sharp internal corner, a spline in hardened tool steel, or a die for stamping, you route the part to EDM.
The two EDM processes are wire and sinker. Wire EDM runs a wire through a hole in the part and cuts a two-dimensional profile — a spline, a gear, a punch, a die plate — with the wire tensioned between two guides. The tolerance on wire EDM is tight — ±0.002 mm and better on modern machines — and the surface finish is fine, because the spark leaves a matte finish that is controllable. Sinker EDM runs a shaped electrode into the part and cuts a three-dimensional cavity — a mould, a coin, a feature with an undercut — with the electrode shape mirrored into the part. The tolerance is similar, the surface is similar, and the electrode is the cost — a sinker electrode is a machined graphite or copper form.
The material case for EDM is the hardened steel. A milling cutter on hardened tool steel — HRC 50 and above — wears fast and the tool life is short; an EDM wire or electrode cuts the same hardened steel without tool wear, because the spark erodes the material without mechanical contact. A die in D2 tool steel at HRC 60 is an EDM part; the same die in soft steel is a milling part, and the heat treatment is the difference. If you specify the heat-treat condition and the hardness, you route the part to the right process.
The facility behind this guide runs wire EDM alongside 100+ CNC milling and turning machines, with Hexagon CMM verification at ±0.002 mm on the EDM features, and Ppk ≥ 1.67 initial on key characteristics and Cpk ≥ 1.33 in production, under ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded), and ISO 14001:2015 (116024/B/0001/UK/En). Specify the geometry — sharp corner, undercut, hardened steel — and ask whether wire or sinker is the routed process. Contact Felipe Iglesias at [email protected] or +86 13126536955 to confirm the EDM routing and the tolerance band.
A 10-minute checklist pass typically removes the ambiguities that cause 80% of sourcing delays.
Cost and Lead-Time Drivers
Quoting edm spark erosion machine is not like quoting a catalog part. The number moves with material, complexity, tolerance, finish, volume and how clean your drawing is. A few levers dominate, and naming them is how you get a real quote fast:
- Setup and fixturing — the hidden cost. A 5-axis cut in one setup beats three 3-axis setups once geometry is complex; fewer re-clamps also means less stack-up error.
- Tolerance stack-up — every tight call-out is an inspection and scrap tax. This is usually a bigger cost driver than the machine hour.
- Material certs and traceability — 316L with EN 10204 3.1 certs and full heat-lot traceability costs more than shop-stock bar; for medical, auto and aerospace it is non-negotiable, so state it up front.
- Secondary operations — anodizing, plating, heat treat, bead blast. Each is a hand-off, a queue and a tolerance risk.
- Volume — prototypes absorb all setup cost per part; production amortizes it across the run.
To get a real number fast: send a STEP file, the material grade, the three tightest tolerances, finish, quantity and target date. Zhuohang Precision Machining Factory turns clean RFQs around quickly because the estimator is not reconstructing your intent from a JPEG.
A Practical RFQ Checklist
A clean RFQ is the cheapest insurance in CNC sourcing. Send:
- The 3D model (STEP/IGES) and a 2D drawing with dimensions and tolerances called out — the model alone is not a spec.
- Material grade and temper, plus any cert requirement (EN 10204 3.1, RoHS, REACH).
- The three tightest tolerances and any GD&T call-outs that drive function.
- Surface finish, coating or anodizing, and which faces those apply to.
- Quantity, target date, and whether first-article inspection / PPAP is required.
Common drawing traps that cost you money:
- Internal corners cannot be sharp — an end mill leaves a radius. Call out a fillet (≥ 0.5 mm) instead of a square corner.
- Hole depth should stay near or below 4× the diameter for twist drilling; deeper holes need gun drills and longer lead times.
- Walls thinner than ~0.5–1.0 mm chatter and distort. Thicker is cheaper and more stable.
- Standard threads under ~M2 / #2 are fragile in soft metals — avoid unless the assembly demands them.
- Tight tolerances cost money on every feature. Tighten only the surfaces that mate or seal; leave the rest at ISO 2768.
- Heat-treated parts move. If flatness matters post-hardening, plan a finish-grind operation and say so in the RFQ.
Zhuohang Precision Machining Factory reviews drawings for manufacturability before quoting — if a tolerance is needlessly tight or a corner impossible to cut, you will hear about it up front, not at rejection.
Talk to Our Engineering Team
Edm spark erosion machine shows up wherever a part must be both precise and produced in quantity: robotics and automation frames, semiconductor and medical fixtures, e-bike and drivetrain components, aerospace brackets, and consumer-electronics housings. The common thread is a tolerance or a material that punishes a sloppy process.
For each of these, your job is the same: define the function (what must align, seal or bear load), then let the shop propose the cheapest process that meets it. Over-specifying is the quiet budget killer.
How to decide: a practical framework for edm spark erosion machine
When the spec sheet is ambiguous, fall back to this four-step loop. It is how a disciplined shop quotes, and how you should evaluate the quote:
- Function first. List what the part must do — align, seal, bear load, dissipate heat. Every tolerance ties to one of these or it is optional.
- Pick the simplest process that holds true tolerance. 3-axis before 4-axis before 5-axis; turn before mill-turn; machining before EDM. Each step up is a cost you must justify on the drawing.
- Name the material by grade, not family. '6061-T6' not 'aluminum'; '316L' not 'stainless'. The grade sets machinability, certs and price.
- Demand evidence of control. Cpk targets, FAI reports, mill certs. If the shop cannot produce them, the low price is borrowing against your shipment.
Run this loop before you ask for a quote and you will write a better RFQ, get a tighter number, and bore a shop that fits.
An illustrative scenario
To make the trade-offs concrete, consider a representative part — a 200 × 150 × 20 mm aluminum bracket with six M5 bosses on one face and two precision slots on an adjacent face, called out at ±0.05 mm. The thinking is generic and mechanism-based; it is not a specific customer job:
- A 3-axis center machines the top face and bosses in one setup. The two slots on the side need a second setup — acceptable at ±0.05 mm, because the re-clamp error stays well inside the tolerance budget.
- If those slots were called out at ±0.003 mm (milling) / ±0.002 mm (turning), the re-clamp alone would risk the number. That is the moment a 4- or 5-axis single-setup cut earns its premium, not because the machine is 'better', but because it removes the error source.
- Material is 6061-T6, so no special tooling or coolant strategy is needed; cycle time is dominated by the pocket milling, not the drilling.
The lesson: tolerance drives process choice, not the other way round. Write the loosest tolerance that still functions and you usually get the cheapest capable process for free.
A ready-to-send RFQ snippet for edm spark erosion machine
Copy this into your inquiry and fill the brackets. A complete RFQ is the difference between a real quote in 24 hours and a guess in a week:
Subject: RFQ — edm spark erosion machine

1. Part: [name] | Qty: [prototype / N pcs]
2. Model: [STEP/IGES attached] + 2D drawing with dims & tolerances
3. Material: [grade+temper, e.g. 6061-T6] | Certs: [EN 10204 3.1 / RoHS / none]
4. Critical tol: [3 tightest, e.g. ±0.003 mm (milling) / ±0.002 mm (turning) slots] | GD&T: [list]
5. Finish: [Ra, anodize/plating, faces]
6. Target date: [ ] | FAI/PPAP: [required / not]

Send to Felipe Iglesias — [email protected]
Suppliers quote the drawing, not the keyword. The more precise the brief, the less the shop charges to de-risk it.
What this shop actually runs
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Made for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Made for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Made for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Made for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Made for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ready to move from estimate to part? Send your drawing to Felipe Iglesias at [email protected] or reach +86 131 2653 6955. See your resource center at Resources for RFQ checklists, tolerance guides and material quick-reference — built to save you a wrong turn before you cut metal.
Frequently Asked Questions
What does edm spark erosion machine mean in practice?
In short, It is producing a physical part to a digital model on computer-controlled machine tools, where the real value is repeatable accuracy — the same part, same dimensions, lot after lot. Your question is which configuration reaches the features in the fewest setups.
What tolerance can I realistically expect?
In short, About ±0.003 mm (milling) / ±0.002 mm (turning) on standard features, with ±0.002 mm (grind / wire EDM on critical features). General dimensions default to ISO 2768 unless tighter is called out.
Which material should I choose?
Driven by the application: aluminum 6061-T6 for general lightweight structure, 7075-T6 or titanium where strength rules, stainless 316L for corrosion, brass for easy precision. Name the grade and temper in the RFQ; 'metal' is not a spec.
Continue reading: Cnc contract manufacturer · Cnc router services · Precision plastic machining
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM B209/B209M-21 — Standard Specification for Aluminum-Alloy Sheet and Plate
- ISO 9001 — Quality management systems — Requirements